Sandpaper Jumbo Roll Factory Production Workflow for Wide Abrasive Rolls
2026-09-17
Wide abrasive rolls don’t just happen. Behind every jumbo roll that feeds converting lines for wide sanding applications lies a factory workflow where precision and material science collide. From raw backing unwinding to resin coating, grain deposition, and final curing, each step has to be controlled or the roll fails on the floor. At SHENZHEN SUN ABRASIVES, that workflow is built around repeatability and width consistency, not guesswork. In this post, we walk through the sandpaper jumbo roll factory production workflow, highlighting where quality is won or lost and why wide abrasive rolls demand more than scaled-up narrow line thinking.
The Backing Gets Cleaned, Tensioned, and Primed
Before any coating touches the back of the carpet, the backing fabric goes through a thorough wash. This removes dust, loose fibers, and any sizing left from weaving. Cleanliness here matters because even tiny particles can prevent the latex or polyurethane from bonding evenly. The wash also slightly roughens the surface, giving the later primer more to grip onto.
Once clean, the backing is stretched on a tenter frame. The tension must be perfectly balanced—too tight and the carpet will ripple when released, too loose and the coating will pool unevenly. Skilled operators adjust the clips and chains while watching the weave lines stay straight. This step locks in the carpet's final dimensions before anything is applied.
Finally, a thin primer is rolled or sprayed across the stretched backing. It soaks into the fibers and fills the tiny gaps between warp and weft. The primer acts as a bridge, helping the main adhesive layer stick without bleeding through. After a short drying pass, the backing is ready for the heavier coating that gives the carpet its body and stability.
Resin and Grit Meet on the Coating Line
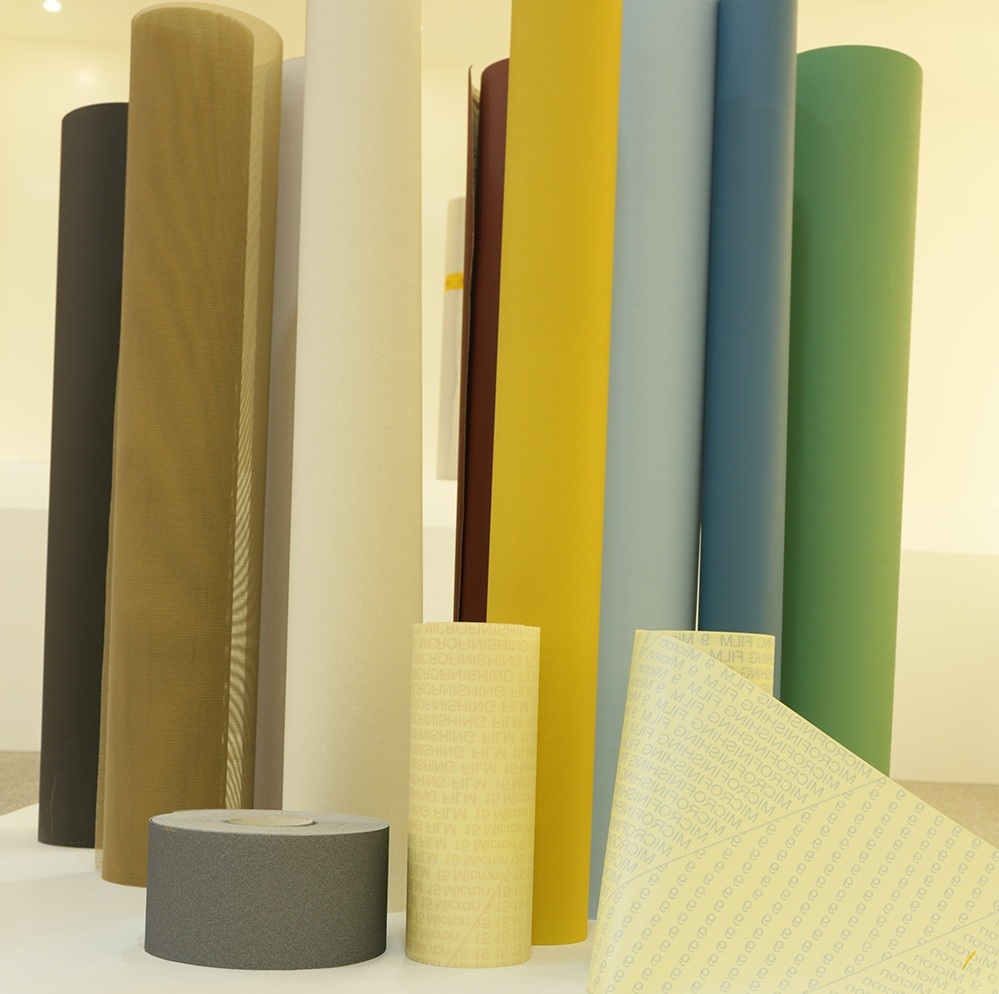
On the coating line, a measured stream of resin flows onto the substrate while a calibrated grit dispenser releases abrasive particles in a controlled curtain. The two components meet just before the curing zone, where a series of leveling bars and air knives work the grit into the wet film. Operators monitor the ratio in real time, adjusting for viscosity shifts caused by ambient temperature or batch variation, so the grain embedment stays consistent from edge to edge.
Once cured, the surface carries a fine, irregular tooth that breaks up water film and gives boots and tires something to bite into. Unlike a smooth epoxy coat that turns slick after a rain, this finish keeps its grip even on loading ramps, wash bays, and stair treads. The resin locks the grit in place, so the texture doesn’t shed or polish away under forklift traffic.
Different grit sizes and resin chemistries can be paired on the same line without retooling—a quick change of hoppers and nozzles shifts the profile from a fine non-skid for pedestrian areas to a coarse anti-slip for heavy equipment zones. That flexibility lets a single coating run produce surfaces tuned to specific safety requirements, while still maintaining a uniform appearance batch after batch.
Drying and Curing in a Temperature-Controlled Tunnel
Operating a drying and curing tunnel with precise thermal regulation changes how moisture leaves a product. Instead of relying on ambient conditions, the tunnel holds a steady temperature band while fans push air through at a controlled velocity. This setup keeps the surface from crusting over too early, which would trap solvents or water inside. Adjusting the ramp rate—often a slow climb over several hours—lets the core reach equilibrium with the shell, reducing internal stress that leads to cracking or warping.
The real advantage shows up in batch consistency. A well-tuned tunnel repeats the same dry-bulb and wet-bulb readings every cycle, so the first item and the last item see nearly identical conditions. Operators can fine-tune airflow direction, switch between horizontal and vertical circulation, or introduce staged humidity drops without opening doors and losing heat. That level of control matters most for thick coatings, cast parts, or food products where a few degrees of drift changes texture, hardness, or shelf life.
Maintenance also gets simpler when curing happens inside a sealed tunnel. Filters catch airborne particles before they settle on wet surfaces, and the exhaust system vents off volatiles rather than letting them condense on walls. Regular calibration of sensors and occasional fan bearing checks keep the environment predictable. Over time, the tunnel pays for itself by cutting reject rates and shortening total cycle times—without sacrificing the slow, even cure that quality demands.
Winding Without Wrinkles or Telescoping
Achieving a clean wind starts with understanding how tension builds across the material. When the incoming web or strand carries uneven stress, the layers settle unevenly, creating the two classic flaws: wrinkles near the core and telescoping toward the flanges. The practical fix is not to simply increase overall tension, but to make that tension consistent from edge to edge and from start to finish. Short, frequent adjustments at the unwind and traverse points do more than one large correction at the drive.
Roll geometry matters just as much as tension. A slightly crowned roller or a carefully aligned lay-on nip can compensate for small variations in thickness that would otherwise accumulate into a soft edge. For narrow or sensitive materials, reducing the traverse speed at the reversal points prevents the material from piling up at the sides, which is where telescoping usually begins. Wrinkles, on the other hand, often trace back to trapped air. A little more time under the nip, or a modest reduction in winding speed, lets each layer settle before the next one lands.
Finally, watch the pattern of the finished roll. If the end face looks like the layers have shifted sideways, the traverse timing or the edge guide likely needs attention, not the core. If the surface shows small creases that repeat every few wraps, the incoming tension profile is the culprit. Making these distinctions early saves material and keeps a winding line running at its intended pace.
Slitting Wide Rolls into Usable Widths
Slitting wide rolls into usable widths is less about simply cutting material and more about matching the cut method to how the web behaves under tension. Large master rolls arrive from mills or coating lines, often too wide for downstream equipment, so they are unwound under controlled tension and passed through a series of circular shear knives or razor blades set at exact intervals. The spacing and depth of these blades are not fixed; they change with material thickness, hardness, and surface sensitivity. A gap that works for 2-mil polyester film may leave ragged edges on 10-point paperboard or generate unwanted dust on a coated nonwoven.
Beyond blade setup, the real challenge is keeping the slit strips uniform from start to finish. That means tension must be actively managed at the unwind, through the slitting station, and at each rewind position. If rewind tension drifts too high, narrow rolls can telescope or develop hard, stretched cores; too low, and they become soft or cinched. Many modern slitting lines use closed-loop feedback to adjust speed and nip pressure on the fly, which helps handle slight variations in caliper or moisture. For delicate films and foils, crush-cut systems often produce cleaner edges with less dust, while thicker laminates and nonwovens are better served by shear-cut blades that slice rather than tear. Keeping the tooling sharp and the alignment true is what ultimately keeps waste low and converting lines running without constant stops.
Inspecting Edges, Coatings, and Package Integrity
Every chip that rolls off the line carries a hidden story in its edges and coatings. A slight burr on the die edge, a micro-crack under the passivation layer, or a faint delamination near the bond pad can turn a promising wafer into a field failure. That’s why technicians don’t just glance at the package—they run a fingernail along the edge, tilt the part under a high-intensity lamp, and scrutinize the coating for any haze, pinholes, or uneven wetting. These subtle cues often reveal stress from dicing, moisture ingress, or a plating bath that drifted out of spec long before electrical testing catches anything.
Package integrity goes deeper than a clean visual. You tap the molded body with a non-marring probe and listen for the dull thud that suggests an internal void. You flex the leads slightly—not enough to deform, just enough to feel for a brittle solder joint or a hairline fracture at the leadframe exit. A quick acetone wipe on the marking area tells you if the ink will survive a board wash. For hermetic packages, you run a fine leak test with helium or a bubble test under fluorocarbon fluid. The goal is to catch that one unit in ten thousand with a compromised seal, because once it ships, it becomes a customer’s line-down.
What separates a routine inspection from a truly useful one is pattern recognition. Maybe the edge chipping always clusters on the south side of the wafer—that points to a worn dicing blade, not random handling. Or the coating thickness varies in a crescent shape, hinting at a spin bowl imbalance. A seasoned inspector logs these observations without being asked, correlating edge roughness with the batch’s singulation pressure or the plating current density. The final sign-off isn’t just a pass/fail stamp; it’s a short note in the traveler that says, “Watch the left-hand magazine—three units showed faint coating pullback near pin 1.” That kind of detail keeps the line ahead of tomorrow’s scrap.
FAQ
Wide abrasive rolls run under much higher web tension across long drying ovens and converting stations. A heavier backing, usually a polyester film or a C-weight paper, resists stretching and necking so the abrasive coating stays flat and the roll tracks straight without wandering.
Grain anchoring happens right after the make coat is applied. The backing passes under a curtain or electrostatic coater that drops or propels abrasive particles onto the wet resin, then a light compaction roller presses them into the adhesive before it moves into the first oven.
Edge control starts with the coating head itself. We use adjustable lip gaps and sometimes edge dams on the knife-over-roll coater, plus a slight crown on the metering roll. Downstream, infrared edge heaters can gel the resin faster at the sides so it doesn't flow toward the center.
A staged cure works better. The first zone might sit around 90–110°C to drive off solvents and level the resin, the middle zone climbs to 130–150°C for crosslinking, and the final zone backs off slightly to avoid thermal shock. Blasting high heat right away causes skinning: the surface cures while volatiles stay trapped underneath.
Splice points are flagged in the inspection system. When the converting line reaches a flagged section, it either slows down and cuts around the splice or marks the finished roll so the customer knows a splice is present. We never ship a splice hidden inside a roll.
We sample both edges and the center of the roll for coating weight, grain adhesion, and tensile strength. A full-width strip is also run over a test drum to check for chatter marks or uneven wear, and the roll is checked for telescoping after a simulated transport vibration test.
Film backings give better tear resistance and more uniform thickness, which matters for fine-grit abrasives used in wet sanding or high-speed applications. Paper is cheaper and works fine for coarse, dry sanding, but film holds up when the roll has to survive repeated flexing and moisture exposure.
Conclusion
A wide abrasive roll begins with a jumbo backing that passes through a cleaning station where dust, sizing residues, and uneven tension are removed before the web is pulled to a consistent width. Operators then apply a thin primer layer to seal the fibres and give the resin something to grip, because without that bond the abrasive grains would shed within the first few metres of use. Once the backing leaves the primer stage, it moves straight onto the coating line. There, a controlled resin film is metered across the surface and the grit is dropped or electrostatically projected into the wet adhesive, which helps orient the sharp edges outward. The amount of resin, the air humidity, and the line speed all shift slightly between grit grades, so the coating team adjusts the settings from batch to batch.
After coating, the web travels through a temperature-controlled tunnel divided into distinct zones. First the solvents evaporate, then the resin gels, and finally the bond fully cures without making the backing brittle. The cured jumbo roll is wound under carefully matched tension to avoid wrinkles, telescoping, or soft spots that would ruin later conversion. Next, the wide roll moves to a slitting line where it is cut into narrower widths for belts, discs, or sheet stock, with edge trimmers removing any thin or ragged margins. Throughout the process, inspectors check coating weight, edge straightness, and package integrity, marking any roll that shows uneven grit distribution or loose wrapping. This combination of controlled priming, coating, curing, winding, slitting, and inspection is what keeps wide abrasive rolls consistent enough for industrial sanding jobs.
Contact Us
Contact Person: Amanda Wang
Email: [email protected]
Tel/WhatsApp: +86-13602569854
Website: https://www.sunabrasives.com.cn