OEM Bead Wire Ring Production Line Explained for Tire Manufacturers
2026-10-07
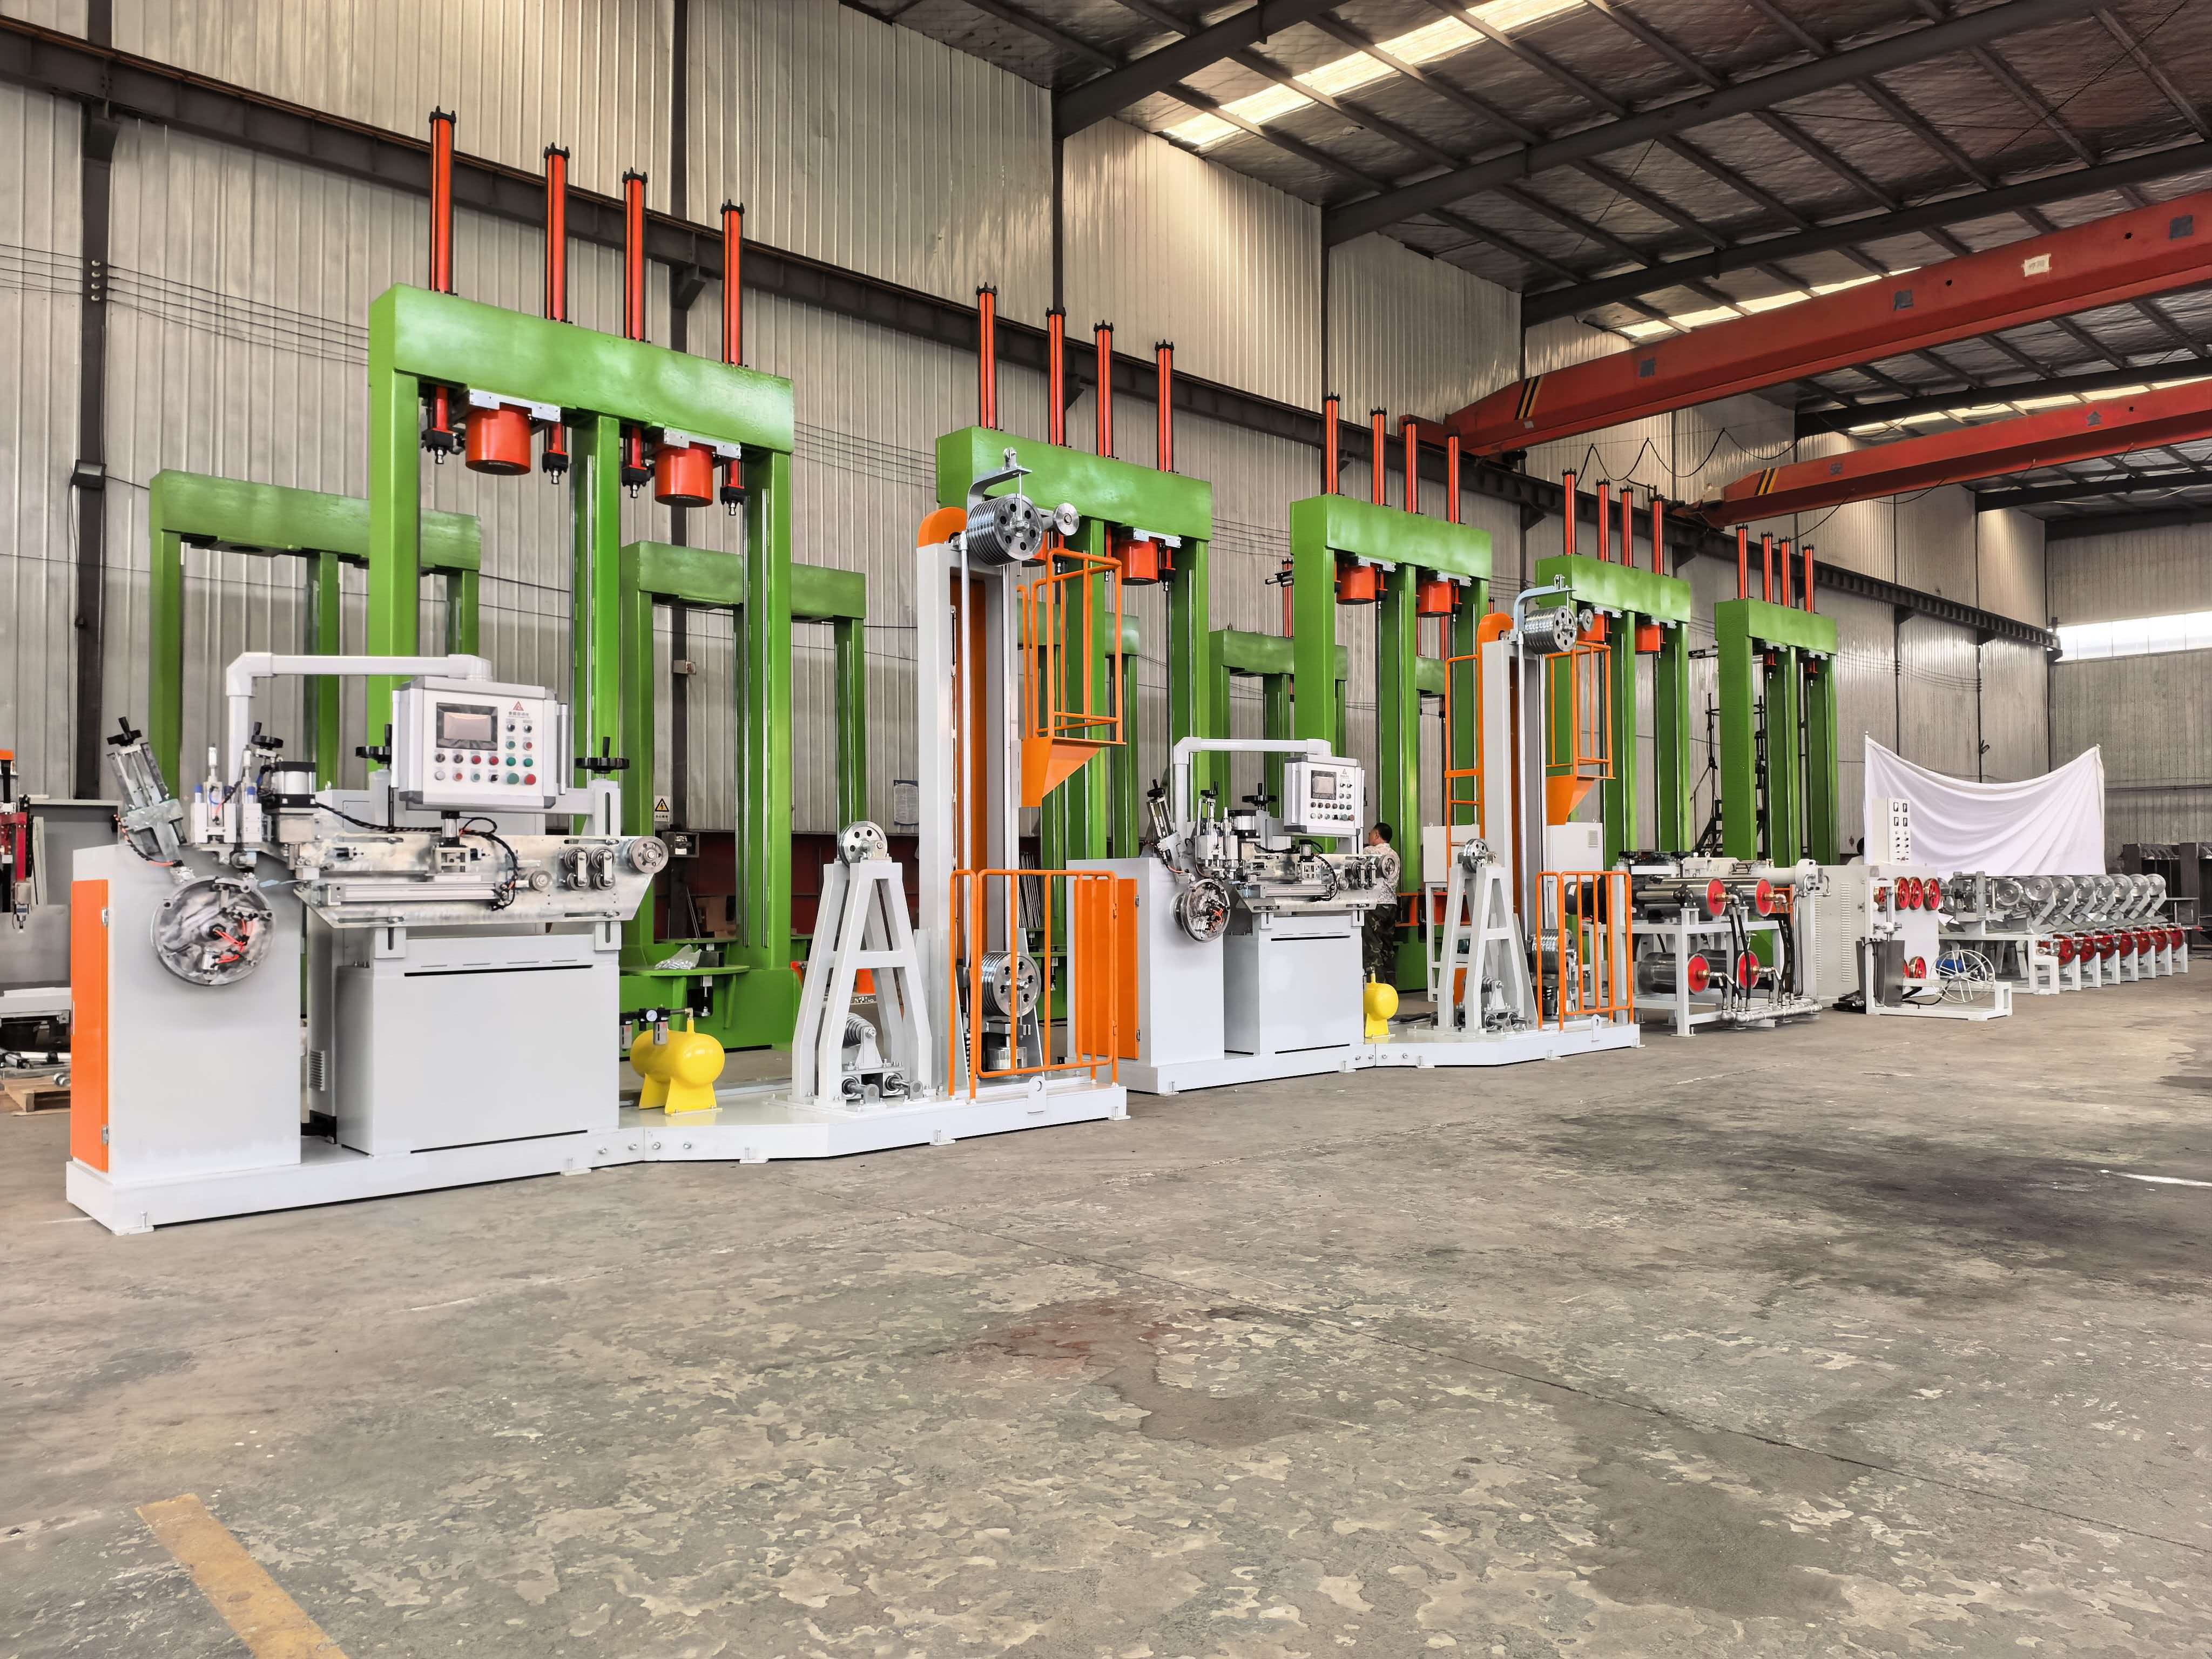
Every tire depends on a part most drivers never see—the bead wire ring. It keeps the tire seated on the rim under load, heat, and speed. But for tire manufacturers, producing these rings at OEM volumes without losing precision or uptime is a daily challenge. AUGU AUTOMATION approaches this differently. This post walks through how an OEM bead wire ring production line actually works, where the usual bottlenecks hide, and what to look for before your next line upgrade.
Where Raw Steel Wire Becomes a Precision Bead Ring
The journey from raw steel wire to a precision bead ring isn't a single leap but a series of deliberate, almost obsessive transformations. It starts with wire that arrives dusty from the mill, straight but unremarkable. In our shop, that wire goes through a custom rolling process that changes its cross-section just enough to catch light differently, then gets cut into blanks on a machine older than most of our staff—and we keep it because it still holds tolerance better than anything new. No two batches behave exactly the same, so we adjust feed speeds and die pressures by hand, listening for the faint squeal that means the metal is fighting back.
What separates a bead ring you notice from one you overlook is how the join disappears. After forming the ring, we don't just file the seam; we anneal it in a small nitrogen-purged kiln, then work the surface through three grades of abrasive before a final polish. That's where the precision actually lives—not in the spec sheet, but in the absence of any visible interruption. If you run a fingernail over the seam and feel nothing, we've done our job. If you feel even a whisper of a step, it goes back into the fire and starts over.
Of course, raw steel wants to rust, and a ring meant for daily wear can't hide behind a coating that wears off in a month. So we pass the finished rings through a steam treatment that builds a thin oxide layer, then seal it with a food-safe wax that soaks into the pores. The result isn't a shiny chrome look—it's darker, quieter, almost organic. That's deliberate. We want the ring to age with the hand that wears it, not against it. Precision here doesn't mean sterile; it means knowing exactly how much imperfection to leave in place.
Why Bead Ring Geometry Decides Tire Fit and Safety
The angle and radius of the bead ring do more than just help a tire slip onto a rim. They determine how evenly the bead seats against the rim flange, which directly controls how well the tire holds air under load and during cornering. A bead that sits too loose may creep and leak, while one that bites too aggressively can make mounting dangerous and damage the rubber at the rim junction.
Variations in bead ring contour also shift the stress distribution across the sidewall. If the geometry does not match the rim's drop-center profile, the tire may not center properly at high speed, causing vibration and uneven wear. In extreme cases, a mismatched bead shape can allow the tire to unseat during hard braking or emergency steering, which is not a theoretical risk but a real safety failure.
Modern tubeless setups rely on a tight, repeatable interference fit between the bead ring and the rim seat. This is not only about keeping air inside; the bead ring’s cross-section also affects how force transfers from the axle to the contact patch. A well-designed profile preserves that connection even when tire pressure fluctuates, while a poorly matched one turns a simple pothole hit into a sudden loss of control.
Automation That Keeps Bead Rings Consistent Without Overspending
Many workshops assume that holding bead ring tolerances within a few thousandths of an inch requires a six-figure robotic cell. In practice, a simple pneumatic collet closer paired with a used PLC often delivers repeatable clamping force and jaw alignment at less than a tenth of that cost. The key is pinpointing the exact forming or drilling step where variability creeps in, then automating only that station instead of reworking the entire line.
Machine vision doesn't have to mean industrial-grade smart cameras. A $200 USB microscope camera and open-source contour detection scripts can measure outer diameter and roundness in real time, flagging any ring that drifts outside the acceptable band before it reaches the next operation. This closed-loop check replaces slow manual sampling and cuts scrap without adding a dedicated quality control shift.
Another overlooked lever is quick-change tooling designed around a shared datum. Instead of buying separate machines for each ring size, a single actuator can swap preset mandrels and guides in under a minute. Storing the parameters for each size in the PLC means no re-tuning after changeovers. The result is consistent output across a product family while the automation budget stays tied to the actual defect sources, not to vendor hype.
The Overlooked Step: Stress Relief and Coating Before Winding
Most coil failures don’t start with the wire itself. They start with what happens to it before a single turn goes on the form. Drawing, stranding, and shipping all leave the conductor in a stressed state—tiny bends and micro-fractures that aren’t visible but will show up later as hot spots or shorted turns. A controlled anneal or low-temperature bake lets those internal stresses relax before the winding begins. Skip it, and you’re building a part with a built-in fatigue timer.
Coating is the other half of that same quiet prep work. A thin, even layer of varnish or enamel does more than insulate—it locks the conductor geometry in place and prevents adjacent turns from abrading each other under vibration. The trick is applying it after stress relief but before winding, so the coating isn’t cracked by the expansion and contraction that happens during the bake. Done this way, the film stays intact, and the coil’s thermal and mechanical life gets noticeably longer.
How to Spot a Bead Wire Line That Will Cost You Later
Look for uneven spacing or sudden kinks along the wire's path. A bead wire that sits flat and holds consistent tension rarely causes trouble, but a slight wave or a few strands separating under light finger pressure are early signs of internal fatigue. These small irregularities grow into hard spots that snap without warning.
Check the coating at every splice and sharp bend. A healthy line keeps a smooth, unbroken surface. If you see cracks, dull patches, or a fine powdery residue, the protective layer is already failing. Moisture gets underneath and eats the steel from the inside, so the wire loses strength long before any visible break shows up.
Measure both sides of the bead at three or four points. A difference of more than a hair means the line has started to deform unevenly. That kind of stretch won't correct itself. It might hold for another season, but under hard braking or a fast corner, it turns into a sudden failure that costs far more than replacing the wire early.
From Coil to Finished Ring: A Walk Through the Real Process
Most rings start life as a wide, tightly wound coil of steel strip. The first step is slitting that coil down to widths that match the ring’s eventual cross‑section. Then the narrow strip is fed through a series of roll‑forming stands, each one bending the metal a little more until it takes on a circular profile. It’s a gradual, almost sculptural process—too aggressive a bend at any single stage and the material will kink or work‑harden unevenly.
Once the circle closes, the ends are flash‑welded or laser‑welded under pressure. The resulting joint is rough, so it goes through a scarfing or grinding pass to knock down the weld bead. After that, the blank is reheated in a controlled furnace and quenched, then tempered to relieve internal stress. This is where a ring stops being a bent strip and begins to behave like a single, homogeneous part.
The last stage is precision sizing. The ring is pressed over a series of mandrels or rolled between dies to refine its diameter and roundness. Skiving or honing may remove a few microns from the bore, and a final surface treatment—phosphate, zinc, or oil—adds corrosion resistance. By the time it’s packed, the original coil has been cut, shaped, welded, hardened, and measured into a part that will hold a bearing, seal, or shaft under real working loads.
FAQ
It takes coated steel wire and turns it into precise circular rings that keep the tire seated on the rim. The line handles unwinding, straightening, forming, cutting, and welding or splicing, then delivers finished bead rings ready for the tire building stage.
Wire tension control and the forming or welding step have the biggest impact. If tension drifts, diameter and ovality go out of spec. A stable joint at the weld or splice keeps the ring from failing under inflation stress later on.
Most modern OEM lines support quick changeovers, but within a practical range. Servo-driven forming heads and adjustable guides let operators change diameters in a few minutes. Switching wire gauges, though, usually calls for different straightening rollers and updated welding parameters.
Because bead rings carry tight tolerances for roundness, joint strength, and coating adhesion. An OEM-specific line builds in automatic diameter checks and weld inspection, which cuts scrap and reduces the amount of manual rework needed.
You start seeing rings with inconsistent diameters, off-center welds, scratched coatings, or occasional wire breaks during forming. These issues often come from worn guides, misaligned straightening rollers, or weld cooling that isn't working as it should.
Automated coil loading, in-process diameter measurement, and automatic reject sorting keep the line moving with fewer people watching it. Real-time trend data also helps predict when a forming tool or weld electrode needs replacing before it causes an unplanned stop.
Key factors include the required bead diameter range, wire tensile strength and coating type, target production speed per hour, maximum acceptable changeover time, and whether inline vision inspection or data logging is needed for traceability.
Yes, but the configurations differ. Passenger tire lines typically focus on higher speed and smaller diameters, while truck tire lines need to handle heavier wire gauges and stronger welds. Some manufacturers offer modular stations so a line can be upgraded as production needs change.
Conclusion
Turning raw steel wire into a precision bead ring is less about rolling metal into a circle and more about controlling every variable that most people never see. The wire arrives in coils with its own memory, hardness variations, and surface condition. The production line has to straighten, cut, and form it into a ring whose diameter, roundness, and weld integrity are held to tolerances that tire makers can't compromise on. A bead ring that's slightly out of round or has an uneven weld won't seat properly on the rim. That translates into slow leaks, vibration at highway speed, or worse. So the geometry isn't a cosmetic detail; it's the difference between a tire that fits every time and one that becomes a warranty claim. Modern lines use servo-driven forming heads and laser measurement to correct deviations in real time, but the smartest setups don't chase perfection with expensive add-ons. They build consistency into the mechanical path itself, which keeps costs down without letting a single bad ring slip through.
What often gets skipped in cheaper lines is stress relief and coating before the wire is wound. If the steel retains forming stress, the ring can spring open slightly after welding, pulling it out of spec days later. A proper in-line annealing or heat treatment step, followed by a thin, even coating of bronze or adhesive primer, is what lets the rubber bond to the bead during curing. Without it, you get corrosion starting at the weld or poor adhesion that shows up only after the tire has been in service. Spotting a line that will cost you later means looking for shortcuts: no closed-loop tension control, minimal cooling after welding, or a coating bath that isn't filtered. Walk the real process from coil to finished ring and you'll see it's not one dramatic machine but a sequence—payoff, straightening, cutting, forming, welding, stress relief, coating, winding, inspection. Each step has to hand off to the next without forcing the operator to babysit it. That's what separates a line that runs a full shift unattended from one that becomes a daily headache.
Contact Us
Contact Person: Lareina
Email: [email protected]
Tel/WhatsApp: +86 17561696737
Website: https://www.auguauto.com/