High Output HDPE Pipe Machine: What You Need to Know for High-Volume Production
2026-10-19
When production demands outpace standard machinery, a high output HDPE pipe machine becomes the backbone of your operation. But not all systems are built for the relentless pace of high-volume manufacturing. From melt uniformity to cooling efficiency, small design differences can mean thousands of meters lost—or gained—every week. In this guide, we’ll walk through the critical factors that separate true workhorses from bottlenecks, and why industry leaders are turning to COMRISE for extrusion lines that keep their numbers climbing.
Where High Output Claims Fall Short in Real Runs
Manufacturers love to advertise peak output numbers measured in controlled lab conditions, but real-world performance tells a different story. Temperature swings, fluctuating power draw, and less-than-perfect input materials all chip away at that theoretical maximum. What you see on the spec sheet rarely survives contact with a dusty workshop or a humid afternoon.
Wear and tear also plays a quiet but relentless role. Bearings loosen, filters clog, and seals degrade, each shaving off a few percentage points of output without any obvious warning. The machine that dazzled in the first week may settle into a comfortable, lower plateau after a month of daily use, and most users won't notice until they compare records.
Then there's the matter of consistency. High output claims often focus on a brief burst rather than sustained performance. Run the equipment for a full shift, and thermal throttling or voltage sag can force it to back off. Factor in routine maintenance pauses and the need for frequent cool-downs, and the effective throughput ends up far closer to ordinary than remarkable.
The Melt Pressure Problem Nobody Mentions
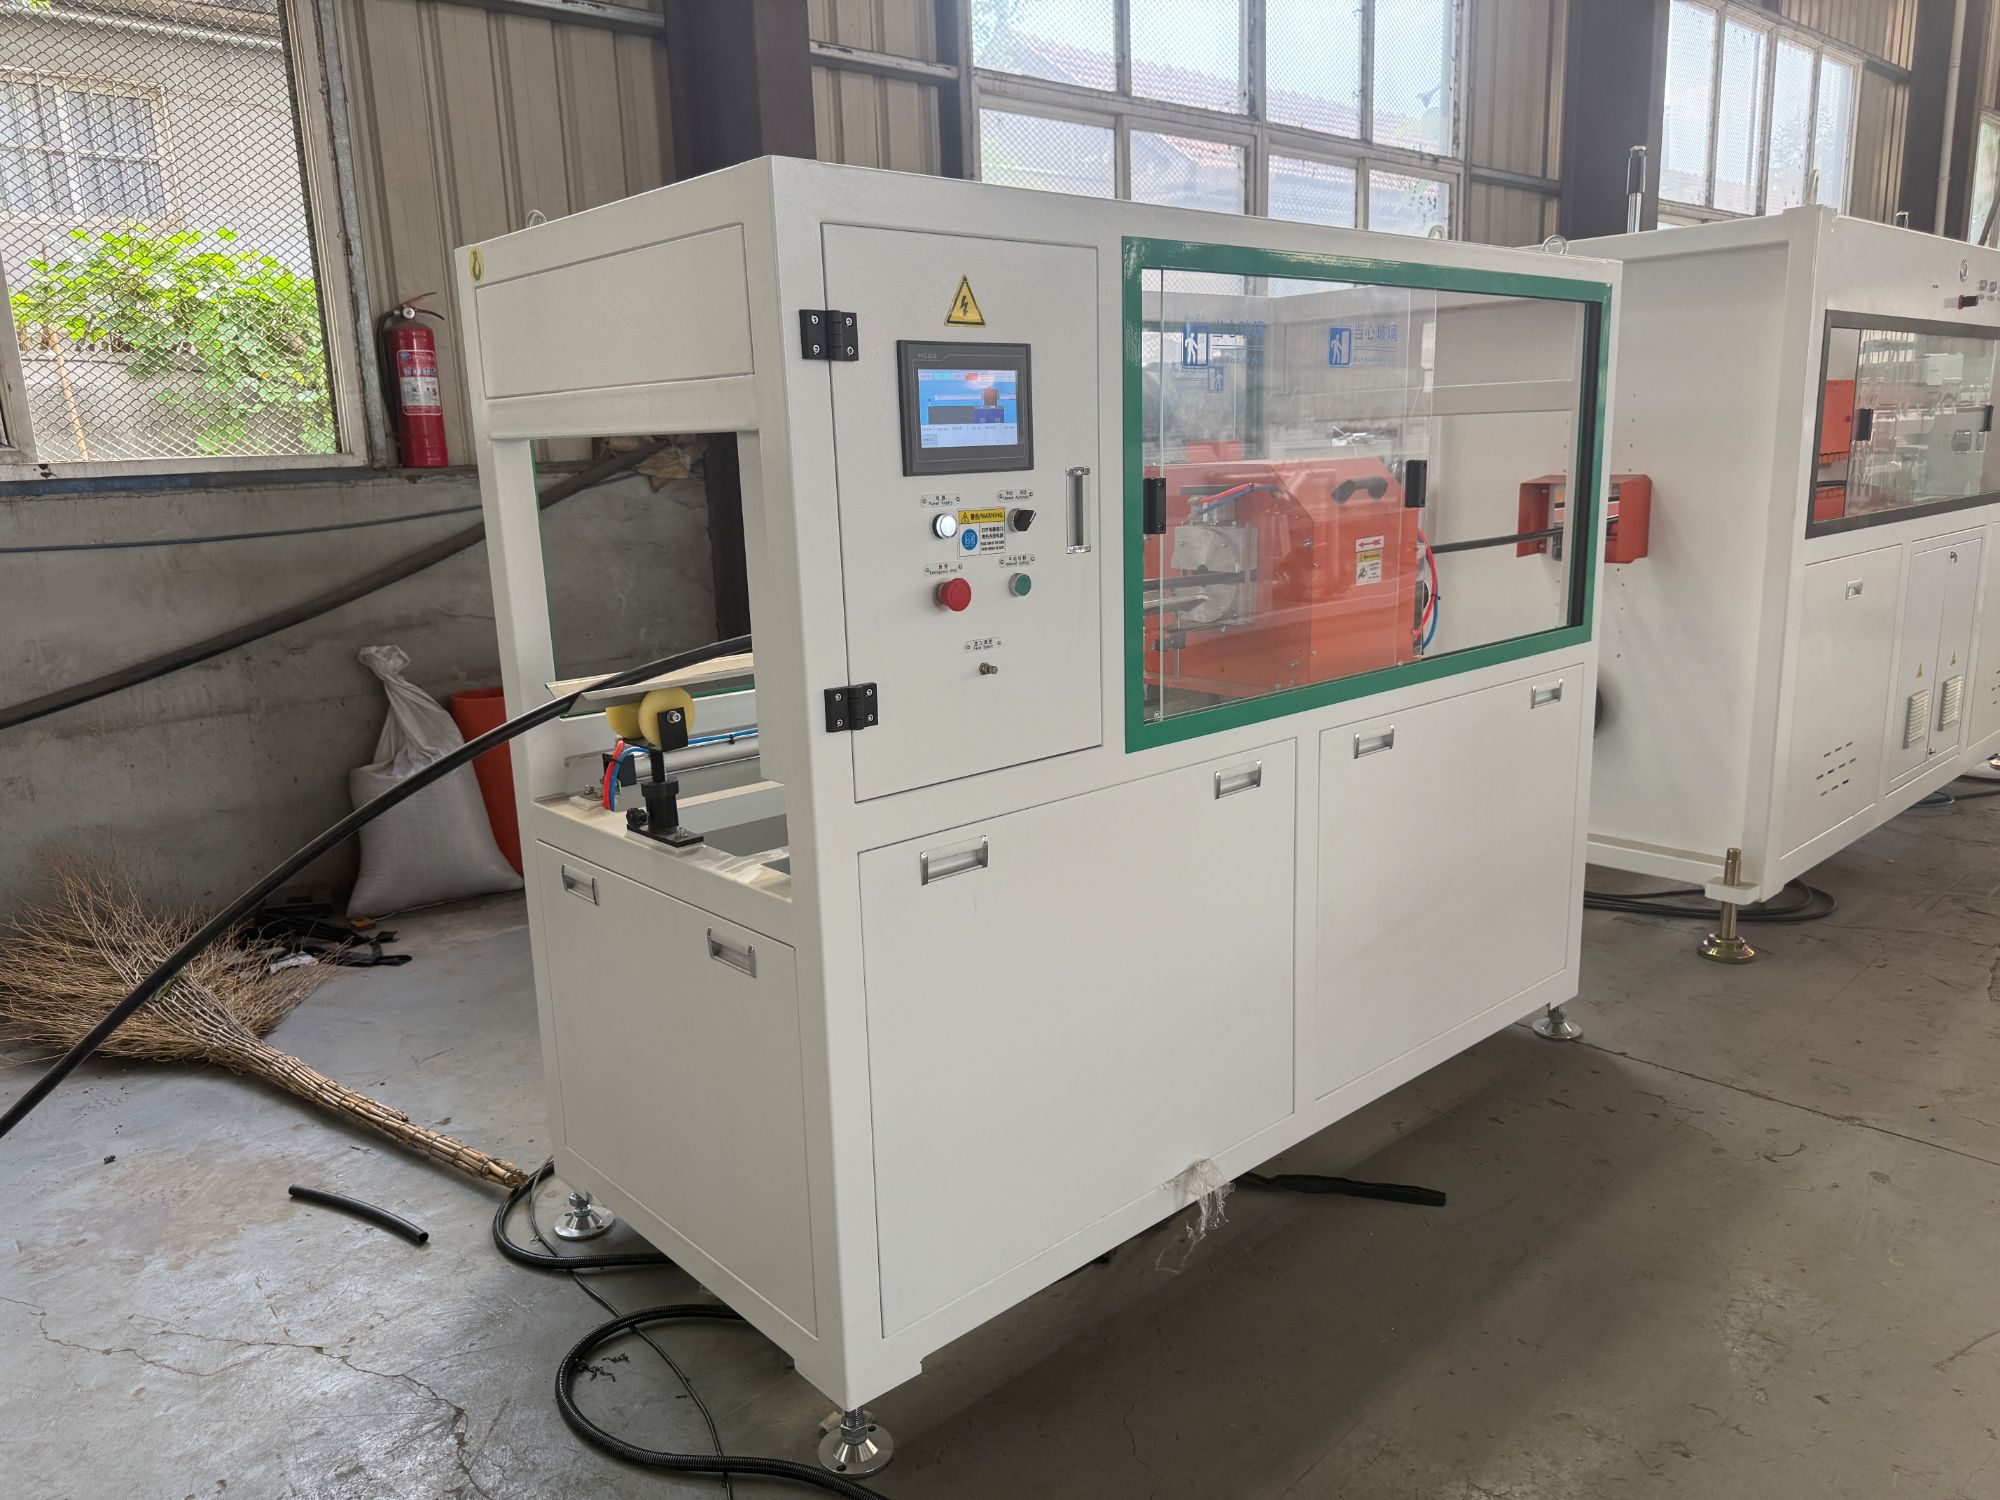
Ask any extrusion line operator about melt pressure and you'll get an earful about setpoints, barrel zones, and screen pack changeouts. But almost nobody mentions the quiet drift happening inside the pressure transducer itself. It doesn't fail with a bang—it loses calibration by a few percent each month, and the controller happily accepts the wrong reading as truth.
The root cause is usually the diaphragm or the fill fluid behind it. At sustained temperatures above 300°C, the fluid expands, contracts, or begins to break down. A tiny scratch from abrasive filler only makes the leak path easier. The reading still sits within the normal range, so alarms stay silent while melt pressure at the die actually sags or spikes, turning dimensional control into guesswork.
The fix isn't complicated, but it requires attention nobody wants to spend. Cross-check the transducer with a portable gauge during routine maintenance, and replace the fill fluid on an interval instead of waiting for burnout. Keep a spare sensor calibrated and ready so a comparison test takes ten minutes, not a full shift.
Screw Geometry Tweaks That Add Tonnage Without Extra Wear
A small increase in feed-section channel depth on a single-stage screw—typically 0.5 to 1.2 mm on a 90 mm barrel—lets the screw pull in more pellets per revolution without raising screw speed. That matters because higher rpm is the usual wear trigger for root and flight edges. Keeping the depth change conservative avoids breaking the solids bed into a melted film too early, which otherwise chokes the channel and drops output per turn.
Barrier flights in the transition zone also help. Setting the barrier clearance around 0.10 mm allows molten material to pass while holding back un-melted granules, so the screw can use a slightly higher compression ratio without forcing hard particles against the barrel wall. The result is better melting efficiency at the same screw torque, not extra abrasion.
On the metering end, shortening the land length of a Maddock-style mixer by about 30% and opening its clearance by 0.02 to 0.04 mm cuts pressure drop across that section. Lower pressure drop means the same motor load can drive 10 to 15 extra rpm, which directly translates to more tons per hour without the wear that comes from pushing into a high-pressure dead spot.
Why Faster Haul-Off Speeds Do Not Equal More Pipe
In pipe extrusion, the haul-off unit is often mistaken for the throttle that controls production rate. The reasoning seems straightforward: if the pipe moves through the line faster, you get more meters per minute. But that logic breaks down because the molten tube leaving the die has a fixed volume per unit time based on extruder output. Pulling it faster doesn't magically add material; it simply stretches the same volume over a longer length, which reduces wall thickness and can pull the outer diameter out of tolerance. The result isn't more saleable pipe—it's scrap or downgraded product.
True throughput gains come from increasing the extruder's melt output and ensuring the downstream cooling and sizing can handle the higher mass flow. If you boost haul-off speed without those changes, you end up fighting the calibration sleeve, creating surface defects, and setting residual stresses that show up later as poor impact resistance. So the haul-off speed is a synchronization parameter, not a production lever. It must match the melt output and cooling rate; otherwise, faster is just a faster way to make bad pipe.
Energy Draw at Peak Throughput: What Your Utility Bill Will Not Tell You
Most facilities only see the monthly total on their bill, but that number obscures the sharp spikes in current that occur when equipment runs at full speed. At peak throughput, motors, compressors, and drives can pull two to three times their average load for short bursts. These transient draws rarely register as a separate line item, yet they force transformers and cables to operate near their thermal limits, accelerating insulation aging and increasing the odds of unexpected downtime.
Another hidden cost comes from poor power factor during heavy load periods. Utilities often apply a penalty or adjust the measured demand based on reactive power, but the exact formula is buried in tariff fine print. A facility can be billed for capacity it never actually used because the utility has to size its upstream equipment for the worst-case instantaneous draw, not the monthly average. This means two sites with identical energy consumption can pay very different demand charges simply because one has a smoother load profile at peak output.
The real danger is that these inefficiencies compound quietly. Wiring losses increase with the square of the current, so a brief surge at peak throughput can waste far more energy than the same amount of work spread over a longer period. And because the bill only reports aggregate kilowatt-hours and a single demand figure, operators rarely see the correlation between production scheduling and the hidden costs of running everything at once.
Matching Downstream Cooling to a Hotter, Faster Melt Stream
Faster line speeds and higher melt temperatures push more thermal energy into the downstream cooling section every minute. A water trough or calibration sleeve that once kept the product within tolerance may now leave the core soft or the surface rippled. Matching cooling to this hotter, faster melt stream rarely means simply adding more length. It usually calls for rethinking how heat is transferred from the extrudate to the cooling medium. Turbulent water flow, direct spray impingement, and staged temperature zones can all raise the effective heat transfer coefficient without creating a massive footprint.
The first few seconds after the melt exits the die are especially critical. If the surface is quenched too aggressively, a frozen skin forms while the interior is still molten, which can lead to voids, warpage, or residual stress. A better approach is to use a short air gap or a warm first bath to allow some relaxation, then follow with high-intensity cooling once the product has enough mechanical strength to handle the thermal shock. For semi-crystalline polymers, the cooling rate also affects crystallinity and shrinkage, so the downstream setup needs to be tuned not just for heat removal but for the final morphology the part actually requires.
FAQ
It's not just a bigger motor. High output machines use longer screw designs, optimized barrel heating zones, and often twin-stage cooling to push more kilograms per hour without over-shearing the melt. You'll typically see throughputs above 600 kg/h for 250-630 mm pipe, with some lines reaching 1,200 kg/h or more depending on the extruder size.
Most high output lines are designed around a diameter range, not a single size. A well-built setup with quick-change die heads and adjustable vacuum tanks can switch between 110 mm and 400 mm or 250 mm and 630 mm without replacing the whole downstream. The real limit is the haul-off pulling force and the sizing sleeve diameter.
Cooling is usually the bottleneck, not the extruder. You need enough chilled water flow and a vacuum spray tank long enough to remove heat from thick HDPE walls. If your cooling capacity is under-sized, the pipe comes out with internal stress, ovality, or surface defects, and you end up slowing the line anyway.
High output lines are less forgiving with recycled or mixed pellet feeds. You want MFI stability within a tight band, low moisture content, and minimal fines. Many operators add an on-line gravimetric blender and a desiccant dryer even for virgin HDPE because small feed variations get amplified at 800-1,000 kg/h.
Look beyond the extruder motor rating. A well-insulated barrel, efficient AC drives, and barrel heating with ceramic or induction elements can cut total kWh per kg by 15-25%. Ask suppliers for a guaranteed specific energy consumption under your target pipe diameter, not just the max load.
With high output lines, you can't manually adjust every parameter fast enough. Closed-loop thickness control, automatic die centering, and laser or ultrasonic diameter gauges let one operator manage the whole line. The best setups also log all process data for traceability and let you recall recipes for different pipe classes with a single tap.
Yes, the haul-off and vacuum tanks are long and heavy. You need a level floor with sufficient load capacity, and sometimes a pit for the water circulation system. Also plan for enough headroom if you're running large diameter pipe with a stacking or coiling unit at the end.
Focus on the screw and barrel wear, especially if you use any recycled content. Check screw clearance every 1,500-2,000 hours, replace or rechrome the barrel before it affects output, and keep the vacuum pump water filters clean. A minor drop in throughput from wear can wipe out the cost advantage of high output quickly.
Conclusion
High-output HDPE pipe machines look impressive on paper, but actual run data often tells a different story. Claims fall short where melt pressure gets ignored: once screw speed crosses a threshold, pressure at the die becomes unstable, causing wall thickness swings and melt fracture that force operators to slow down anyway. Screw geometry is the real lever—subtle changes like a longer feed section, adjusted compression ratio, or redesigned barrier flights let you push more kilograms per hour without increasing screw wear, but these are rarely changed on standard machines. That means the bottleneck isn't always the extruder itself; it's how the screw interacts with the resin at high throughput.
Haul-off speed is another misleading metric. Pulling pipe faster only works if the cooling line can remove heat at the same rate. A hotter, faster melt stream hitting a short cooling tank produces oval pipe, shrink-back, and internal stress. Energy draw at peak throughput compounds the problem: running heaters and drives flat-out drops efficiency, and your utility bill will show a much higher cost per kilogram than the brochure suggests. High-volume production demands matching the entire line—screw, melt pressure stability, haul-off rate, cooling capacity, and energy input—rather than chasing one number.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com