Eco-Friendly Purification Panel Production Line for Sustainable Clean Air Manufacturing
2026-09-21
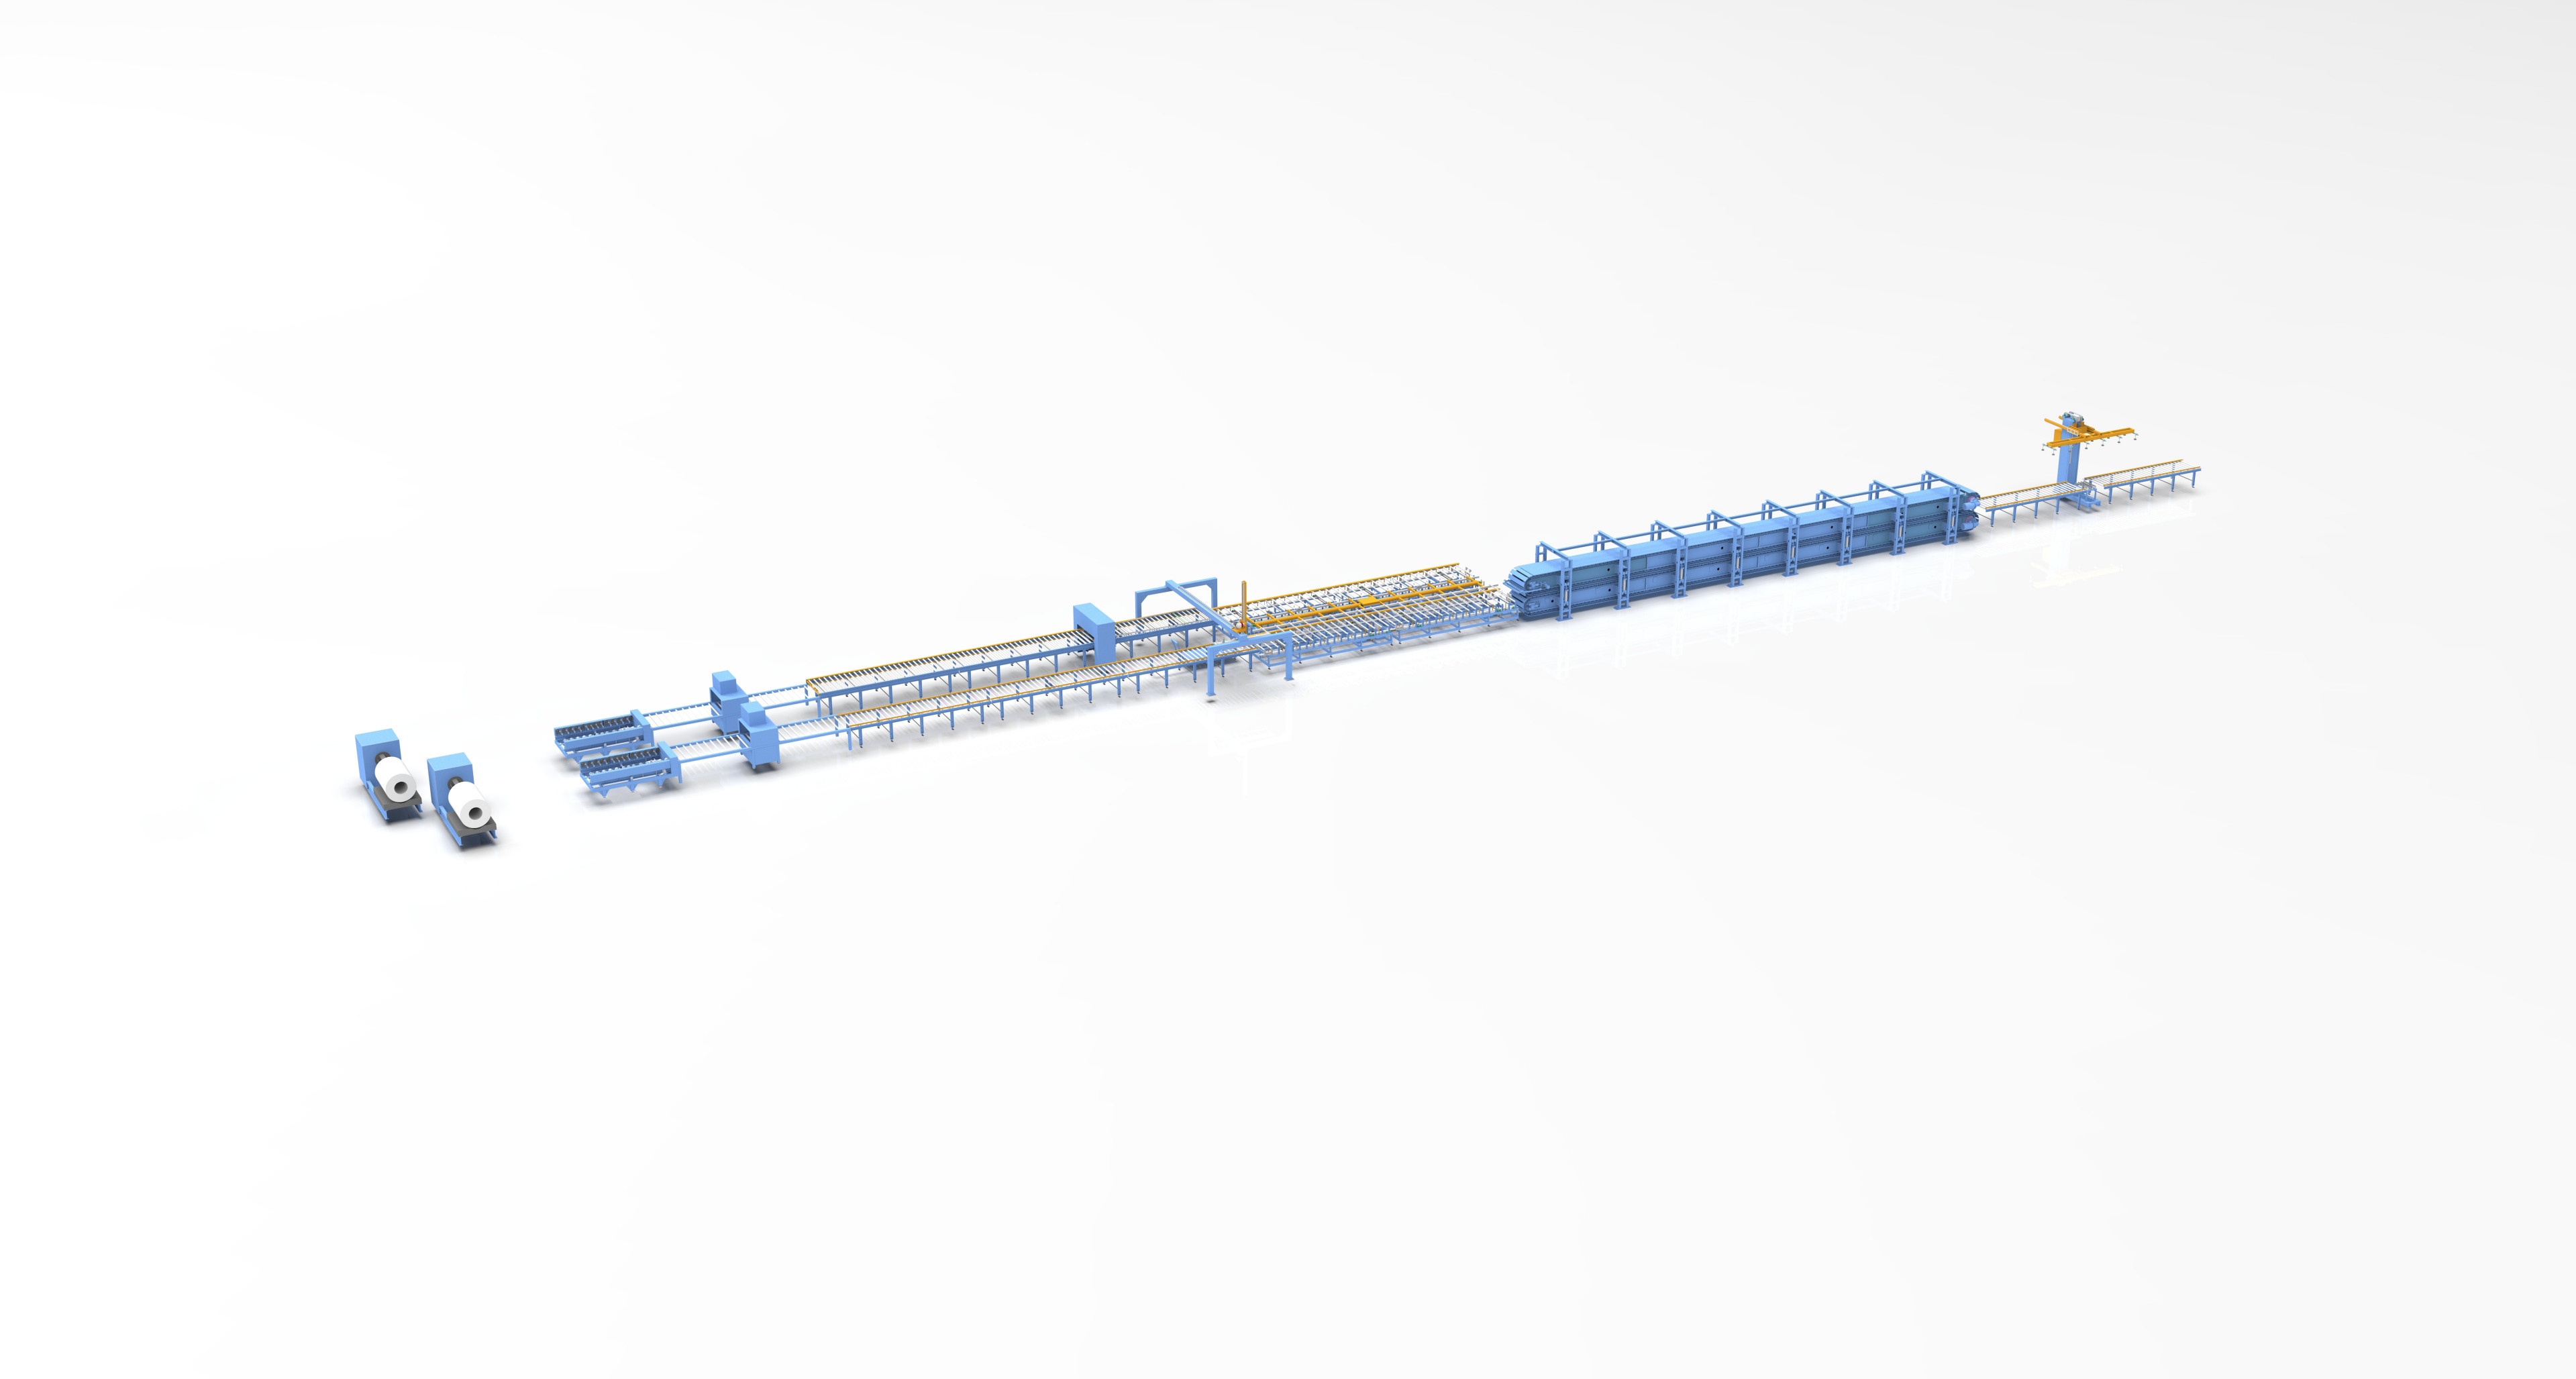
What if the equipment used to manufacture clean-air panels was itself clean? That question drives the eco-friendly purification panel production line at YI ZHOU TECHNOLOGY. Instead of bolting on filtration as an afterthought, we engineered the entire process—from raw material handling to final assembly—to minimize waste, emissions, and energy use. In this post, we'll walk through how that line works and why it matters for sustainable manufacturing.
Rethinking Raw Inputs for Cleaner Panels
Most discussions about panel maintenance jump straight to cleaning schedules and chemical mixes, but that overlooks a quieter variable: the raw materials feeding the surface in the first place. Dust composition, water mineral content, and even the micro-abrasives carried by wind differ wildly from one site to another. Instead of treating every panel as a blank slate, we should audit what actually lands on the glass before choosing a removal method.
Field observations show that a significant share of soiling comes not from ambient dirt but from the residues left by previous cleaning cycles. Hard water spots, detergent films, and brush micro-scratches accumulate into a stubborn layer that traps further particles. Rethinking the input means questioning the purity of rinse water and the hardness of contact materials. A softer, lower-mineral approach can often reduce the need for aggressive scrubbing later, extending the panel's optical clarity with less intervention.
There is also a material dimension: some panel coatings respond poorly to certain solvents or alkaline cleaners, creating a chemical haze that cuts light transmission over time. By mapping the exact contaminants at a site—whether pollen, industrial fallout, or salt spray—teams can shift from generic washing to targeted, low-impact removal. This upstream focus on raw inputs turns cleaning from a routine chore into a precision task that preserves panel efficiency for years rather than months.
Energy Cuts That Don't Compromise Output
Most plants treat energy reduction as a trade-off with throughput, but the real opportunity sits inside operating curves, not capacity limits. Fine-tuning compressed air pressure bands, staging chillers around partial loads, and running pumps on variable frequency drives often recovers 10–18% of energy spend without touching line speed or batch size. The trick is matching supply to actual demand minute by minute instead of holding fixed setpoints out of habit.
Another overlooked lever is sequencing. Shifting energy-intensive but non-bottleneck tasks to off-peak windows, preheating with waste heat from compressors, and shutting down idling conveyors between shifts keeps output identical while slicing base load. Operators who log interval data rather than monthly totals usually spot these cuts within a few weeks, because the waste hides in transitions and standby states that rarely show up on a summary dashboard.
Designing Out Waste Before the Line Starts
Most waste isn’t created on the factory floor—it’s baked in long before anyone touches a tool. When a part gets designed with an odd offcut pattern, or a fastener is specified that requires three extra handling steps, the line inherits those problems. Designing out waste means treating the CAD screen as the first workstation. It’s where you ask: can this shape nest tighter? Can this joint be reached without flipping the assembly? Small choices there ripple into material savings, shorter changeovers, and fewer bins of scraps that never needed to exist.
One of the quietest ways to do this is to stop designing parts in isolation. A bracket that looks elegant on its own might force a supplier to mill away sixty percent of a blank. Talk to the people who actually cut, bend, and assemble before the first prototype. Let them redline the geometry early. Often a five-millimeter tweak or a switch to a commercially available thickness removes an entire finishing step. That kind of feedback doesn’t slow the project down—it keeps rework from showing up later as line stoppages or rejected batches.
There’s also value in pretending the line already exists while the design is still fluid. Walk the sequence in your head: material arrives, gets nested, cut, formed, joined, inspected. Where does something get clamped twice? Where does offal pile up? If you can name those spots before tooling is ordered, you can change the geometry or the process instead of bolting on recovery systems afterwards. The goal isn’t a perfect drawing; it’s a drawing that lets the line run clean on day one.
Keeping Plant Air Clean While Panels Cure
Curing panels release a steady stream of solvents and resin fumes that can settle into every corner of a production floor. Rather than relying on a single oversized exhaust fan, many facilities find better results by positioning low-velocity intake vents near the curing racks and letting air drift naturally toward the far wall. This slow, directed movement traps odors close to the source before they have a chance to spread, keeping the rest of the plant breathable without creating cold drafts that could affect panel quality.
Another overlooked factor is the timing of air exchanges. Running the filtration system at full speed only during active curing misses the long tail of off-gassing that continues for hours after the panels are moved. A simple schedule upgrade—running the scrubbers for two additional hours after the last batch leaves the oven—can lower the average airborne concentration dramatically. Pairing this with frequent filter checks means the air stays cleaner without a jump in energy use.
For plants that struggle with stubborn resin smells, adding a thin layer of activated carbon matting inside the return ducts often makes a noticeable difference. The mats are easy to cut to size, cost little to replace, and capture the smaller vapor molecules that standard particulate filters miss. Combined with keeping curing zone doors closed except during loading and unloading, this approach keeps the working environment fresher without redesigning the entire ventilation layout.
The Closed-Loop Details Most Lines Skip
Most production lines treat closed-loop control as a checkbox: sensor wired up, PID gains tuned at commissioning, and then nobody touches it again until something breaks. What they miss are the small, unglamorous behaviors that quietly degrade performance over weeks and months. For example, the feedback signal itself often drifts. Thermocouples age, pressure transducers lose calibration, and encoders pick up mechanical backlash that isn't in the original model. These shifts are slow enough that the loop still appears to work, but the process drifts farther from its intended setpoint, forcing operators to make manual corrections that never get fed back into the system.
Another skipped detail is actuator deadband and response asymmetry. A valve that takes 300 milliseconds to respond in one direction and 800 in the other can cause the controller to overshoot or hunt, even if the tuning constants were perfect on paper. Lines rarely map this asymmetry because it requires a step test that interrupts production. Instead, they widen the deadband or lower the gain, which hides the problem but sacrifices precision. The result is a line that runs “stable” but wastes material, energy, or cycle time because the closed loop is fighting an unmeasured characteristic of its own hardware.
Finally, the interaction between adjacent loops gets ignored. A temperature controller and a cooling water valve might each tune fine in isolation, but when they operate together, the heat exchanger’s thermal lag couples their dynamics. You get a low-amplitude oscillation that never trips an alarm but shows up in increased variance of the final product. Capturing this requires looking at cross-correlation between loops or running a small perturbation test during a planned shutdown. Most lines skip that because it doesn’t fit into a standard maintenance checklist, yet it’s exactly the kind of detail that separates a merely functional line from one that holds tolerance hour after hour without operator intervention.
Scaling Up Without Trading Away Air Quality
Expanding production capacity used to mean accepting a thicker haze on the horizon. That trade-off no longer holds. A growing number of facilities are pairing new lines and bigger freight volumes with electric arc furnaces, hydrogen-ready burners, and closed-loop scrubbers that strip out particulates before exhaust ever reaches the stack. The result is more output per square foot and measurably cleaner air at the fence line—not because regulators forced a slowdown, but because the economics of waste heat recovery and filtration have flipped in favor of tighter controls.
The shift is most visible in port and logistics hubs, where diesel idling has long been the default. Shore power hookups, automated yard tractors, and route optimization now cut nitrogen oxide emissions even as container throughput climbs. Meanwhile, a handful of industrial corridors have started tying expansion permits to real-time fenceline monitoring, so a facility's right to grow depends on keeping benzene, sulfur dioxide, and PM2.5 within a narrow band. That turns air quality from a compliance afterthought into an operating parameter, much like temperature or pressure.
There is no single technology doing the heavy lifting. Electrostatic precipitators, amine-based carbon capture on flue gas, and low-NOx burners each handle a piece of the puzzle, but the real lever is integration. Plants that scale up cleanly tend to treat emission limits as design constraints rather than retrofits. When a new production hall or turbine goes in, the scrubber and heat recovery loop are sized for peak load from day one. That approach avoids the familiar cycle of expansion followed by enforcement action, and it leaves surrounding neighborhoods with something rare: a bigger employer and a lighter respiratory burden at the same time.
FAQ
It goes beyond slapping a green label on the machinery. The line uses water-based adhesives instead of solvent-heavy ones, which slashes volatile organic compound emissions during lamination. The curing ovens run on variable-frequency drives that trim power use by up to 30 percent, and scrap panels are ground down and fed back into the core material stream. Even the packaging station uses recycled cardboard spacers rather than foam.
Any facility that struggles with airborne contaminants gets a direct benefit. Hospitals and clinics need panels that trap pathogens without emitting formaldehyde. Electronics cleanrooms demand ultra-low particle shedding. Schools and office towers want better IAQ to reduce sick days. Food processing plants also use these panels to keep mold spores and grease aerosols out of ventilation paths. The line's flexibility lets it serve all of these without retooling.
It's a mix of precision and reuse. Laser-guided slitting keeps edge trim to under two millimeters, and that trim gets collected, shredded, and blended into the panel core at a controlled ratio. The core itself uses a honeycomb structure made from recycled PET bottles, which actually improves rigidity per kilogram compared to solid fiberboard. Automated density sensors adjust the compression pressure in real time, so you don't get weak spots or over-compressed brittle zones.
Yes, and that's one of the main reasons buyers choose it over fixed-purpose machines. The media feed system accepts rolls from 10 to 50 millimeters thick, including activated carbon cloth, melt-blown polypropylene, and nanofiber mats. Changeover takes around 20 minutes because the guides and tensioners are servo-driven with saved presets. Thickness adjustment is just as quick — the calendar gap and adhesive application rate recalibrate automatically from a recipe database.
Daily, operators should wipe down the adhesive nozzles and check the vacuum belt for fiber buildup. Weekly, you need to inspect the slitting blades and replace them if the edge quality starts to feather. Monthly, calibrate the density sensors and clean the oven's heat exchangers. Every six months, replace the hydraulic filters and check the servo motor couplings. With that routine, the line typically runs 6,000 hours a year with less than two percent unplanned downtime.
Absolutely. The panels coming off this line meet or exceed requirements for LEED v4.1 low-emitting materials, WELL Building Standard feature 04, and California's CDPH Standard Method v1.2. Because the line itself uses water-based adhesives and captures dust at the source, the factory floor also stays below OSHA permissible exposure limits for particulates and formaldehyde. Third-party testing labs can verify the panel emissions within 14 days of production.
Most operations see a full payback in three to five years, depending on local energy prices and waste disposal fees. The energy savings alone from the variable-frequency ovens and LED curing typically cut 18 to 22 percent off the utility bill. Scrap recycling eliminates about 40 percent of landfill costs. Add in the premium price that low-VOC panels command in the market — often 15 to 25 percent higher — and the financial case gets pretty compelling without relying on government subsidies.
Conclusion
Rethinking raw inputs for cleaner panels starts well before any machinery fires up. Instead of defaulting to solvent-heavy resins, the line pairs low-VOC binders with recycled fiber cores that would otherwise land in a landfill. That switch alone shifts the entire curing chemistry toward fewer off-gassing events. Energy cuts are equally direct: variable-frequency drives on the forming and cooling stations ramp down during idle stretches, and waste heat from the curing ovens pre-warms incoming air streams. Output doesn't dip because the line re-tunes cycle times around thermal mass, not peak wattage. Designing out waste before the line starts means every off-cut from panel sizing is re-ground on site and fed back into the core mat, while edge trims are sorted by polymer type for reuse rather than swept into a general bin.
Keeping plant air clean while panels cure comes down to capture at the source. Each curing zone has its own low-velocity hood that pulls volatiles into a biofilter bed, not just a carbon canister that needs replacing. The biofilter's microbes actually consume the VOCs, so there's no spent media trucked off site. The closed-loop details most lines skip include condensate recovery from the dryer exhaust: that water is filtered and returned to the humidity control system, cutting both water intake and discharge permits. Scaling up without trading away air quality means the line's modular extraction ducts are sized for the next expansion from day one. Additional curing bays plug into the same negative-pressure header, so doubling capacity doesn't create dead zones where fumes linger.
Contact Us
Contact Person: Sophia Jiang
Email: [email protected]
Tel/WhatsApp: +86 17367381818
Website: https://yzwelding.com/