Bulk Shoe Eyelets: The Complete Guide to Choosing and Buying in Large Quantities
2026-09-06
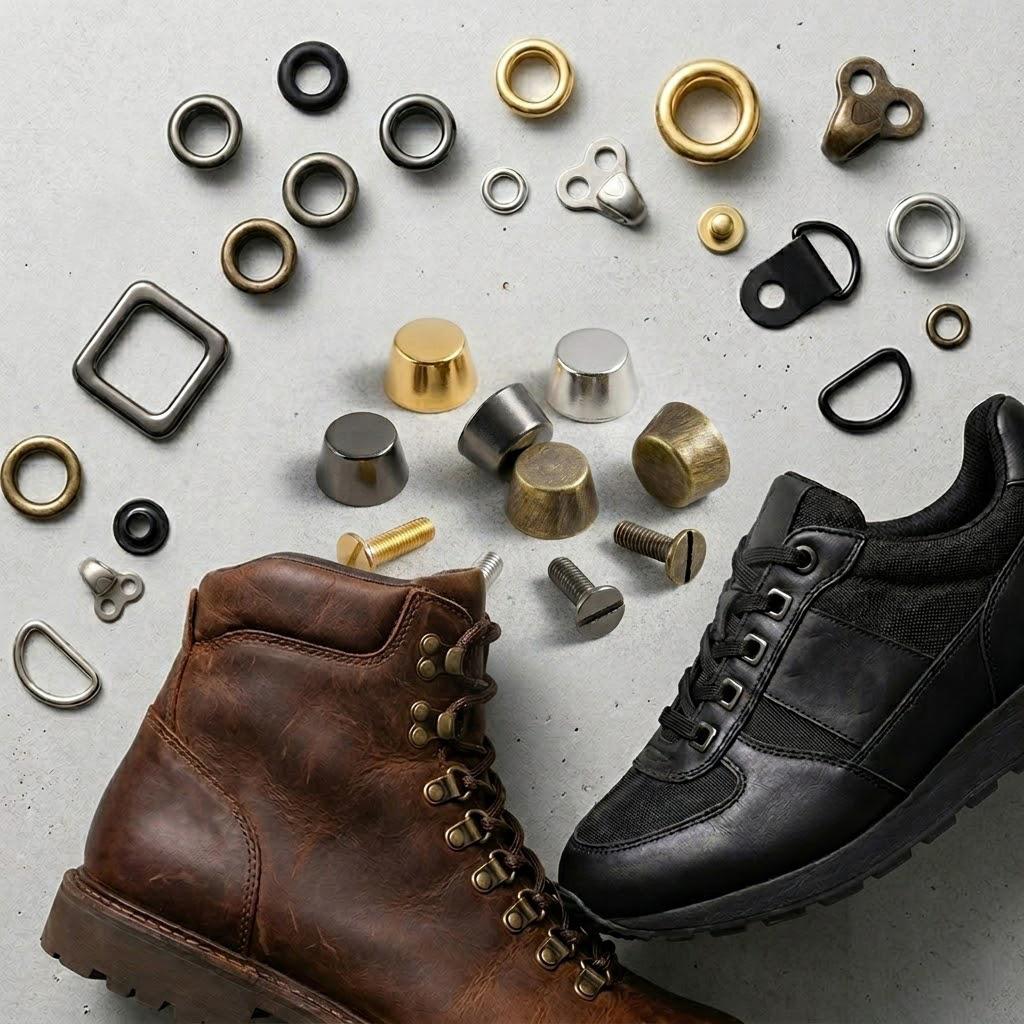
When you're ordering shoe eyelets by the thousand, the wrong choice doesn't just cost money—it costs production time, customer trust, and your own sanity. Bulk buying sounds simple until you're staring at terms like rolled vs. flat, brass vs. stainless, and wondering if that bargain price hides a tolerance issue. This guide cuts through that noise. Whether you're restocking a repair shop or speccing hardware for a new footwear line, you'll learn what actually matters: material strength, finish durability, barrel length, and how to spot a supplier who won't leave you hanging. Along the way, we'll reference proven options from Kingming so you can compare real specs, not just marketing claims. Let's get into the details before your next purchase.
Material Choices That Hold Up Under Stress
Selecting materials for high-stress applications isn't just about picking the strongest option on paper. It requires a careful look at how a material behaves when pushed beyond its comfort zone—how it deforms, how it absorbs energy, and whether it fails gradually or without warning. Ductile metals like certain steel alloys and titanium offer a valuable trait: they bend and stretch before breaking, giving engineers a visible warning sign long before catastrophic failure. On the other hand, brittle materials such as some ceramics or hardened tool steels may boast high hardness, but they can shatter suddenly under impact or cyclic loading.
Thermoplastics and composites have carved out their own niches under stress. Reinforced polymers, for instance, can be engineered with fiber orientation that directly counters expected load paths, creating parts that are both light and remarkably tough. Yet they bring their own quirks—moisture absorption, UV sensitivity, and temperature-dependent stiffness. The real skill lies in matching the material's failure mode to the application's tolerance for risk. In a gear tooth, you might accept gradual wear but reject brittle fracture. In a pressure vessel, you'd demand leak-before-break behavior over outright rupture.
Beyond static strength, fatigue resistance and stress corrosion cracking often decide long-term survival. A material that handles a single overload may still fail after millions of small cycles, especially in corrosive environments where tiny pits become crack initiation sites. Good choices under sustained stress are those that offer a balance: enough yield strength to resist plastic deformation, enough toughness to blunt a growing crack, and enough environmental resistance to avoid hidden degradation. It's this layered understanding—not a single datasheet number—that separates reliable designs from those that merely look strong on the first day.
Sizing Pitfalls When Moving From Samples to Production
Sample data almost never carries the full weight of production traffic. It gets scrubbed, filtered, and trimmed to fit a demo or a test window, which means the noisy edges—oversized payloads, retry storms, malformed inputs, and slow consumers—are silently dropped. When those edges hit production, they don't just add a few percentage points of load; they often dominate the tail. A service that handles 500 requests per second in staging can crumble at 450 in production because every twentieth request now triggers a downstream timeout that never appeared in the sample.
Memory and connection sizing often rely on average record counts from sampled datasets. The sample shows each request carrying 12 items, so you allocate buffers and connection pools accordingly. But production sees bursts where a single batch carries 800 items, or a long-running stream never releases its handles. Connection pools sized for an average of 80 concurrent clients will exhaust themselves during a deploy or a cache flush when 300 clients reconnect at once. The sample never models those moments of coordinated surge.
Latency profiles shift in ways samples can't capture. In a clean test environment, P99 latency might sit at 80 milliseconds because there is no contention, no garbage collection pressure, and no noisy neighbor on the host. Production piles on multiple tenants, background jobs, and network variance, and suddenly that same code path runs at 220 milliseconds. The fix isn't to trust the sample and hope for the best—it's to run shadow traffic against a production-like topology, gradually widen the rollout, and watch the actual resource curves before committing to a final size.
Finishes That Look Good After Hundreds of Laces
Friction from laces pressing, sliding, and tightening against the same small areas is brutal on shoe finishes. Within a few weeks, most topcoats start to show dull patches around the eyelets or tiny cracks along the flex line where the lace exits. But a handful of finishes—typically a matte polyurethane blend with a slight rubbery give—don't just resist that wear; they settle into it. On a pair of everyday boots laced twice daily for months, the finish around the eyelets stayed uniform, gaining only a faint, even gloss where the lace crosses over. No cracks, no color loss, no raw edges peeking through.
Edge sealing matters just as much as the surface coat. Thick lacquered edges look flawless on a shelf, but the moment a lace saws against them a few hundred times, they chip and leave white scars. The finishes that hold up are almost always applied in several thin passes, then burnished or heat-set until they move with the underlying material. You can feel it when you rub a thumb across the eyelet rim—there's a slight tackiness, not a hard shell. That's the finish flexing instead of fighting the lace. After enough wear, the lace itself often frays or the metal hardware dulls while the finish around it still looks freshly sealed.
What to look for if you want this kind of longevity: skip high-gloss coatings that depend on a thick, brittle outer layer. Matte and semi-matte finishes with a soft hand tend to hide minor abrasions and keep their color. Wax-based finishes also blend scratches easily with a quick buff, though they need occasional reapplication. The real test is simple—pull a lace through the eyelet a few times and watch how the finish responds. If it grabs or feels sticky, it will abrade. If it lets the lace slide with just a whisper of resistance, that's the one that will still look intentional after hundreds of laces.
How to Avoid Overbuying When Minimums Feel High
High minimums push you toward buying more than you need, but the real test is whether you'll actually go through the stock before it becomes a liability. Pull your usage history or realistic demand forecast for the next few months, not the annual total that makes the discount look great. If a vendor wants you to order 500 units and you sell or consume 80 a month, that's six months of cash tied up in boxes. For anything with a shelf life, version updates, or storage fees, the per-unit savings can vanish well before the last item leaves the shelf.
Minimums are rarely carved in stone. Ask about staggered delivery — you commit to the full quantity but receive it in smaller shipments over a quarter or half-year. Some suppliers will also accept a smaller first order at a slightly higher per-unit price, then lower the price once you demonstrate repeat volume. The conversation shifts when you frame it as building a consistent purchasing rhythm instead of a one-off haggling match.
If the supplier won't move, spread the risk. Partner with a non-competing business that uses the same materials, or look for a buying group that pools orders. Splitting a high minimum across a few buyers turns an oversized purchase into a routine restock. And before you sign, ask what happens to the surplus if demand drops by 30%. If the honest answer is that it sits in a corner collecting dust, the order is probably too large no matter how attractive the unit price looks.
Spot-Checking a Pallet Without Losing Your Mind
Nobody rolls out of bed excited to count every box on a pallet. But a decent spot-check doesn't have to be a full inventory nightmare. Grab a clipboard or open a note on your phone, pick three to five random cartons from different layers, and compare their labels against the packing slip. If the first two match perfectly, don't celebrate yet — pull one from the bottom corner where damage hides. The goal isn't to verify every unit; it's to catch the kind of mismatch that makes a warehouse manager sigh into their coffee.
The real trick is making the check fast enough that you actually do it. Set a timer for ninety seconds per pallet. Check the shrink wrap for tears before you cut it, then slice a small flap instead of unwrapping the whole thing. Count what's visible, verify a couple of serial numbers or batch codes, and snap a photo with your phone for later reference. If something looks off — a carton that's too light, a label that's smeared, a pallet that's leaning like it partied too hard — flag it and move on. You're not trying to be perfect; you're trying to avoid the kind of surprise that costs an hour on the dock.
What Actually Drives Bulk Eyelet Prices
Most buyers assume size and quantity set the price, but the metal underneath has a stronger grip on the final number. Brass eyelets carry a premium because copper and zinc markets swing faster than steel indexes, and the exact alloy ratio changes how cleanly the barrel rolls. A zinc-plated steel eyelet can cost half as much as a solid brass one, yet a thin brass plating over steel often lands somewhere in the middle—until the plating thickness and salt-spray rating push the quote up sharply.
Tooling and tolerances quietly separate a standard quote from a custom one. If your order fits an existing die set, setup costs get spread across thousands of pieces. But ask for an unusual flange diameter, a taller barrel, or a specific inside finish, and the supplier has to build or modify tooling—sometimes before a single eyelet is produced. Tight concentricity specs and low burr requirements also slow down stamping speeds, which raises the piece price even when material costs stay flat.
Order volume still matters, but not the way most catalogs suggest. The steepest discounts usually appear when you move from a few hundred to a few thousand pieces, because packaging, inspection, and machine setup stop eating the quote. Beyond that, further drops come in smaller steps, unless you can take mill-run quantities or share a production slot with another customer. Shipping weight, finish type, and whether the eyelets need individual sorting or bulk packing can easily add more to the landed cost than a small change in metal price.
FAQ
For most footwear, brass is the workhorse—it resists corrosion and takes plating well, though raw brass can tarnish if not lacquered. Stainless steel is better for work boots or marine gear because it won’t rust even when the finish scratches. Aluminum is lightweight but too soft for high-stress lace points. Zinc alloy is cheap but can crack if over-crimped. If you’re making canvas shoes or lightweight sandals, a nylon or acetal eyelet may be enough and avoids metal staining on light fabrics.
You can’t fully avoid sampling, but you can narrow it down. Measure your lace diameter and add at least 1.5–2 mm for the inner hole so the lace glides without fraying. The flange (outer rim) should be 3–4 mm wider than the punched hole to grip the material. For barrel length, add the material thickness plus about 1 mm of compression allowance—leather compresses less than foam-backed textiles. Ask the supplier for a dimensional chart and order one set of actual samples before the main run.
Beyond the unit price, watch for tooling fees if you need a custom finish or embossed logo. Surface finishes can vary between production batches, so you may need to pay for a pre-production sample run. Shipping weight adds up fast—brass and steel eyelets are dense. If you’re importing, factor in customs duties and possible inspection fees. Also ask about overrun/underrun policies: some factories ship ±5% quantity, which can mess up your inventory if you’re not prepared.
Nickel-plated brass is the most reliable if the base is polished properly before plating; a thin flash coat will wear through at the lace contact points. For darker tones, black oxide on steel or antique bronze on brass performs better than painted coatings, which chip when the eyelet is crimped. If you need a specific Pantone color, powder coating is more durable than wet spray, but it adds thickness that can interfere with setting dies. Ask for a salt spray test report—anything under 24 hours to white rust is not worth buying for outdoor footwear.
Use a simple acceptance sampling plan. For a lot of 10,000 eyelets, pull 125 randomly from different bags. Check for burrs on the inner edge, uneven plating, cracked flanges, and ovality in the barrel. Measure inner diameter with a pin gauge on at least 25 of those. If more than 2 or 3 fail, reject the lot. Also weigh a full bag against the declared count—weight discrepancies often reveal short packing before you open every bag.
Two-piece eyelets have a separate washer that sits on the back side of the material, spreading the pulling force over a larger area. That matters for soft or thick materials like suede, garment leather, or padded collars where a plain eyelet can pull through over time. Work boots and heavy canvas bags almost always use washer eyelets. Plain eyelets are lighter and cheaper, but they rely on the material itself for support—so if you’re using thin lining, go with a washer.
It’s worth finding a specialist. General metal stamping shops may not understand how eyelets perform after setting—barrel flare, flange curl, and alignment matter more than static dimensions. A shoe hardware supplier will have setting dies to test your exact material stack and can advise on barrel length adjustments. They also tend to stock common sizes, which means lower minimums and faster lead times. If a general factory offers a much lower price, request a crimped sample on your actual shoe upper before committing.
Specify that each bag or box contains an exact count, not an approximate weight—many suppliers pack by weight and the count drifts. Ask for moisture-barrier bags with a zip closure if your storage area is humid. If you run multiple colors or sizes on one production line, have the supplier use color-coded labels or separate inner bags per size. For very high-volume automated setting, some factories can provide eyelets on tape reels, though that’s rare for footwear—most shoe assembly still uses bulk hoppers.
Conclusion
Ordering shoe eyelets in large quantities looks uncomplicated until a shipment arrives with the wrong inner diameter or a finish that rubs off after a month. Material choice sets the baseline: solid brass and stainless steel handle repeated stress from laces without collapsing, while zinc die-cast options save money but can crack under heavy pulls, especially in work boots or children's shoes. When you move from samples to production, sizing often drifts because one factory measures barrel length before flanging and another measures the finished height. Ask for a dimensioned drawing with clear tolerances for inner diameter, barrel length, and flange spread before committing to a full run. Finishes are another hidden failure point—cheap electroplating or paint can look fine in a sample bag but develop flaking or rough edges after a few hundred lace cycles. A simple pre-production test is to yank a waxy or flat lace through the eyelet repeatedly and then check for color transfer, exposed base metal, or abrasion on the lace itself.
Bulk pricing conversations usually focus on minimum order quantity, but overbuying is rarely solved by forcing a lower price per thousand. Instead, ask if you can split the order across multiple finishes or schedule partial deliveries to avoid holding a year of inventory in one size. When a pallet shows up, spot-checking doesn't require unpacking every carton. Pull boxes from the top, middle, bottom, and two opposite corners, then count a small sample from each and measure inner diameter, barrel length, and flange thickness. A quick visual scan under a bright light will reveal inconsistent plating or burrs better than measuring every piece. On price, the raw material cost is often a small slice of the quote—setup fees, plating method, tolerance level, and how often you reorder change the number more. Buyers who chase the cheapest unit cost sometimes inherit higher scrap and more customer returns, so agreeing on a defect rate before production is more valuable than squeezing a few cents out of the invoice.
Contact Us
Contact Person: Jamie Zeng
Email: [email protected]
Tel/WhatsApp: +86 13728219269
Website: https://www.kmhardware.com